Introduction
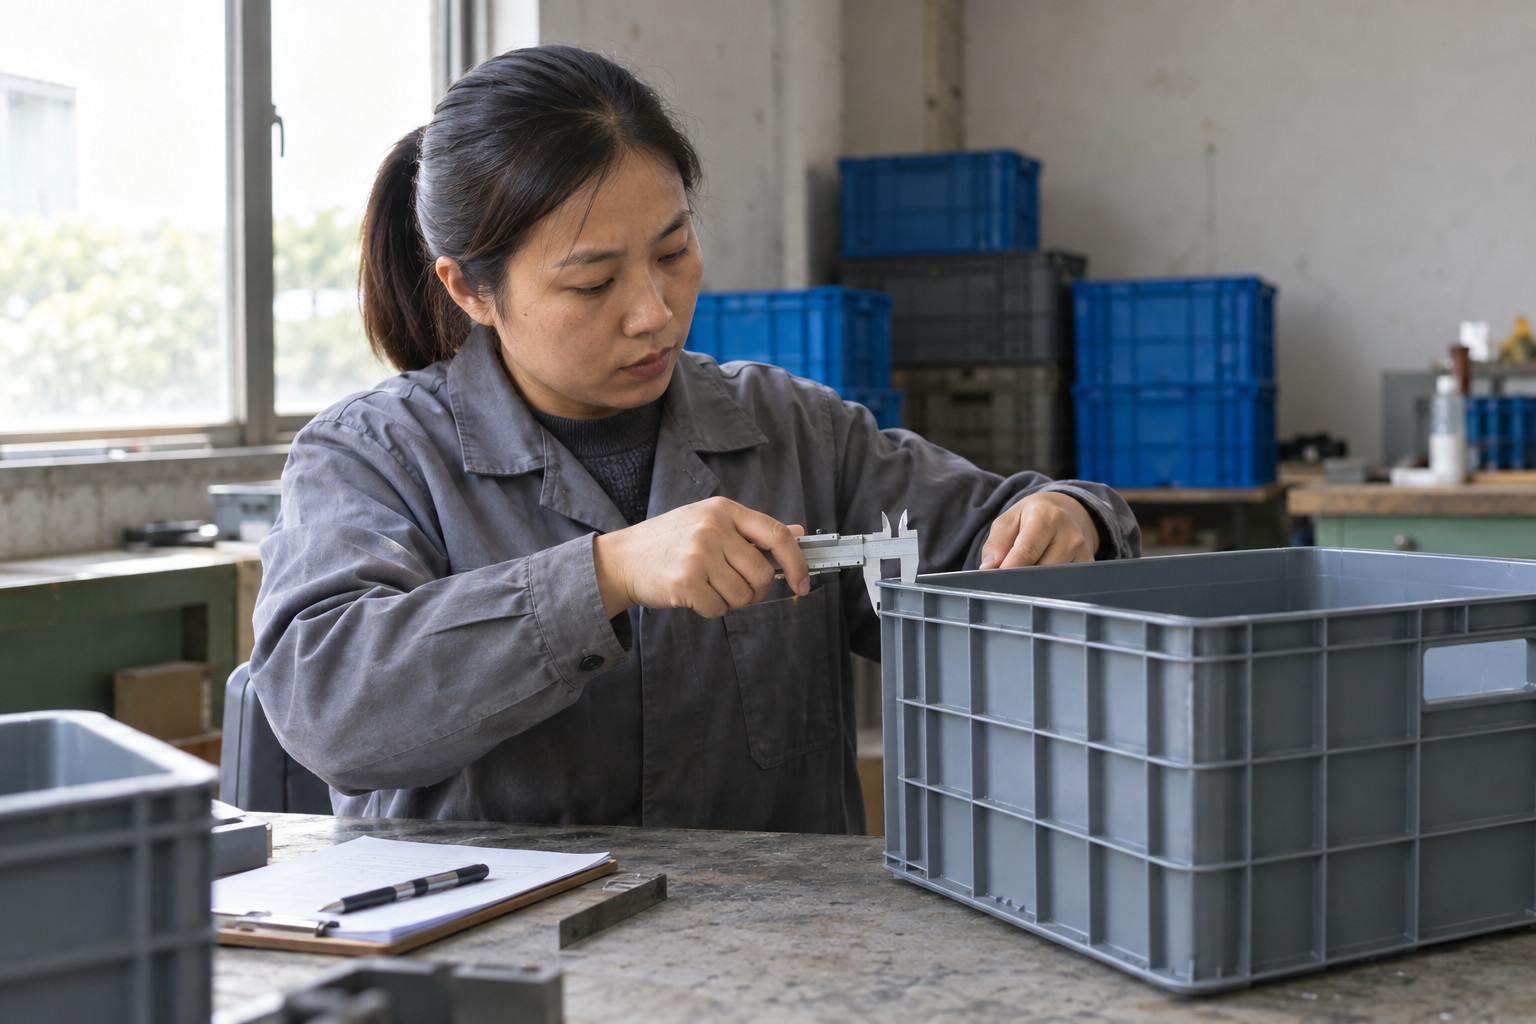
Prevent supplier measurement disputes by agreeing what is measured, where it is measured, how the product is supported, which equipment is used and how borderline results are decided. A nominal dimension and tolerance are only part of an inspection instruction. If the supplier measures a flexible part under tension while an independent inspector measures it relaxed, both may report honestly and still reach different conclusions about the same sample.
For importers and retail buyers, the objective is a repeatable acceptance decision that reflects product application. This guide explains how to build that decision before factory testing or shipment inspection. It does not set universal tolerances or claim that any KudBo product has achieved a particular dimensional result. Numerical examples are hypothetical purchasing illustrations; the appropriate method and limits depend on the actual design, material and function.
Define the Dimension That Matters to the Customer
Start with the consequence of variation. A storage crate may need to fit a shelf opening, nest inside another crate, close securely or stack in a specified arrangement. Those functions do not necessarily depend on the same dimension. Overall width can be useful for logistics, while the position of a latch or mating rim may matter more for assembly. Identify the functional relationship before deciding what to inspect.
When reviewing fold-flat storage crates, distinguish dimensions in the open, folded and assembled states. Specify whether protruding handles or latches are included. If the product must fit an existing fixture, request its available clearance and any relevant variation. A single catalog dimension often cannot answer all these questions, particularly when the product has moving parts or flexible walls.
Use a Drawing or Annotated Photograph
Show the start and end points of each measurement. Label the reference surface and the orientation of the product. A simple annotated photograph can be sufficient for a straightforward consumer accessory, provided it is unambiguous and controlled by revision. For a complex fit, ask an appropriate engineer to provide the necessary drawing and measurement method.
Describe the state of the sample alongside the drawing. Is the lid closed? Are hinges fully engaged? Is packaging removed? Has the product been allowed to recover from compression? These conditions can alter the result without any change in manufacturing. The inspection instruction should make the intended state reproducible rather than relying on what one experienced operator normally does.
Separate Tolerance, Resolution and Uncertainty
A tolerance defines an allowed range in the product specification. Instrument resolution is the increment that can be displayed or read. Measurement uncertainty describes doubt associated with a measurement result. These concepts are related but not interchangeable. A display with many digits does not establish that the measurement method is suitable for a tight purchasing tolerance.
NIST's measurement uncertainty resources provide primary background on evaluating and expressing uncertainty. For procurement, the practical action is to ask the qualified inspection or laboratory team whether the proposed measurement process can support the acceptance decision. Do not select a tolerance merely because it looks precise in a spreadsheet or because an instrument displays that many decimal places.
For a hypothetical dimension specified as 100 millimeters with an allowed variation of 1 millimeter in either direction, the nominal number is not the complete inspection rule. The buyer still needs measurement locations, product condition, suitable equipment and treatment of results near a limit. This example illustrates the questions to resolve; it is not a recommended tolerance for crates, fittings or any other product.
Agree the Method Before Comparing Results
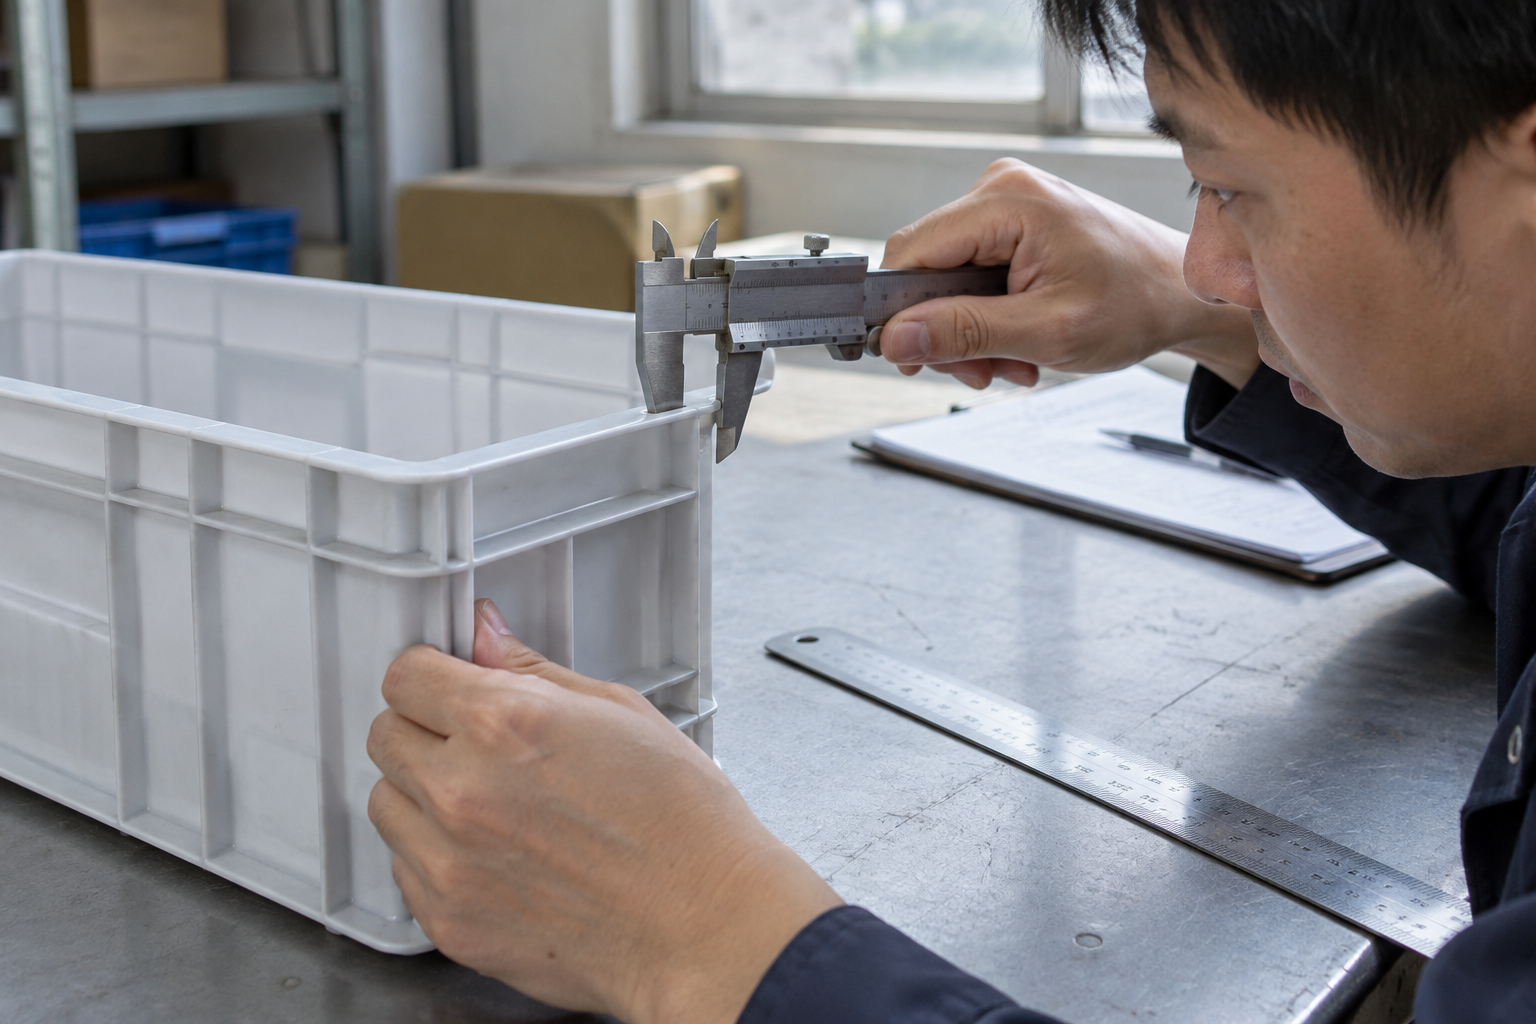
Make a short method sheet for each critical measurement. Include the reference, sample condition, instrument type, contact method, number of readings and reporting units. Explain whether the result is an individual reading, an average or another defined calculation. Averaging should not be introduced after a failure simply because it produces a more convenient answer.
| Method element | Question to settle | Dispute it can prevent |
|---|---|---|
| Reference location | Which surfaces or points define the dimension? | Different operators measuring different features |
| Product state | Open, closed, loaded, unloaded or conditioned? | State-dependent differences |
| Contact force | How is a soft or flexible part contacted? | Compression or stretching differences |
| Equipment | Which range and method are suitable? | Inappropriate tool selection |
| Decision rule | How are near-limit results evaluated? | Retrospective changes to pass criteria |
Address Flexible and Irregular Products
A soft pouch, silicone component or textile organizer may not have one obvious rigid edge. Pulling it flat can change the observed length. Ask the supplier to demonstrate the proposed measurement on a representative sample and record the technique. Where a fixture is used, identify it and explain how it locates the part without distorting the feature being assessed.
For irregular molded parts, decide whether the relevant dimension is a local feature, a maximum envelope or a fit with another component. A convenient caliper position may not represent the customer's use. If several locations must be checked, identify each location rather than permitting the operator to choose a favorable point. A clear method can be more valuable than demanding an unnecessarily tight numerical limit.
Check Equipment and Traceability Claims
Ask for the instrument identifier and evidence that its condition is suitable for the intended measurement. Where calibration records are relevant, check their scope, dates and relationship to the actual equipment used. A certificate for another instrument or an unrelated range does not resolve the question. The inspection provider should explain how it maintains the measurement process between formal calibrations.
NIST's metrological traceability guidance explains that traceability concerns measurement results and their documented connection to references. It does not mean that NIST endorses a supplier or guarantees a product. Avoid turning a phrase such as traceable calibration into a marketing claim that the product itself is NIST approved.
A buyer does not need to become a metrologist to ask useful questions. Request a clear explanation of the measurement chain, relevant uncertainty and suitability for the product tolerance. If the answer is only a certificate image with no link to the inspection method, ask the provider to complete the explanation. Escalate genuinely technical disagreements to a competent measurement specialist.
Mid-Article CTA
Send Your Fit and Inspection Requirements. Share the product, drawing or annotated reference, application, quantity and destination with info@kudbo.com. The KudBo enquiry form can start a discussion about sample evaluation and the measurement questions that should be settled before shipment.
Run a Small Method Alignment Exercise
Before a large order, have the relevant parties measure the same identified samples using the proposed method. Preserve the sample identity and avoid mixing units during transfer. Ask each party to record observations independently before comparing them. The exercise is intended to reveal differences in technique and interpretation, not to manufacture an appearance of agreement.
Compare patterns rather than selecting the most convenient result. A consistent difference may suggest a reference-point or tool issue. Wide variation between repeated readings may indicate difficult positioning, flexible material or an unsuitable process. Discuss these possibilities with the inspection team. Do not automatically average conflicting measurements from different methods and call the disagreement resolved.
Keep Raw Observations
Retain the original readings, setup photographs and notes. A final pass or fail summary can hide useful information about where the disagreement arose. Raw observations also help distinguish a recording error from a physical variation. If a decimal separator, unit conversion or rounding rule caused the problem, correct the record transparently and check whether other reported measurements are affected.
Repeat the alignment exercise when a material, fixture or method changes in a way that could affect results. The amount of work should match the significance of the change. A controlled method is not a permanent guarantee; it is an agreed basis for making comparable observations. Keep revision dates visible so an inspector does not unknowingly use an obsolete instruction.
Decide How Borderline Results Will Be Handled
Near a specification limit, measurement uncertainty can matter to the acceptance decision. Agree a decision rule with the qualified provider before inspection and make its commercial consequences clear. Possible approaches depend on the application and assessment arrangement. There is no universal buyer-friendly rule that removes all risk for both parties.
Do not move the acceptance limit after seeing the results. If a concession is considered for a nonconforming lot, document it as a specific deviation with an authorized decision, affected quantity and any conditions. A concession should not silently become the specification for future orders. Where fit or safety could be affected, obtain the necessary technical assessment before approving any departure.
Define what happens during a disagreement: sample preservation, temporary shipment hold, repeat measurement using the agreed method, and escalation if needed. Assign responsibility for the review and clarify costs in the purchasing arrangement. This makes the process more predictable than an urgent negotiation after the container booking has already been made.
Connect Dimensions With Functional Checks
Passing a dimension does not always prove satisfactory function. A latch may measure within its specified range yet feel difficult to operate because another interacting feature varies. Conversely, an apparently small dimensional difference may not affect the intended application. Use functional checks where they add relevant evidence, while keeping them distinct from the numerical inspection criteria.
For a stacking product, define the intended arrangement and relevant loading conditions with a competent product specialist. For a storage item fitting a shelf, use a representative fixture or documented clearance where appropriate. Do not convert an informal fit demonstration into an unsupported strength or durability claim. Each claim needs its own suitable method and evidence.
Maintain reference samples in a way that preserves their usefulness. The golden sample retention guide covers identification and custody considerations. A retained sample can support appearance and assembly discussions, but it does not replace a drawing or measurement instruction when a numerical limit is the purchasing requirement.
Write a Useful Inspection Report
A dimensional report should identify the purchase order, product revision, lot, sample selection, instrument, method and results. State the units and preserve the number of digits justified by the process. If a result is calculated, describe the calculation. Include departures from the planned method so the buyer understands the limits of the conclusion.
Separate observed defects from hypotheses about their causes. An inspector can report a dimension outside the specified range without claiming to know whether the cause is tooling, cooling, assembly or storage. Root-cause work may require additional evidence. Keeping these statements separate prevents an inspection report from becoming an unsupported diagnosis that drives the wrong corrective action.
For the next order, review whether corrective actions changed the drawing, process or method. Update the relevant revision and communicate it to every party performing the check. If the only improvement is that people now measure the same feature consistently, record that honestly. A reduction in disagreement is valuable, but it is not proof of improved manufacturing capability without supporting data.
Work Through a Borderline Fit Example
Consider a hypothetical folding crate that must enter a customer's shelf opening. The purchasing drawing specifies an external envelope in the fully assembled state. One inspector measures across the body, while another includes a protruding latch. Their numbers describe different things. Resolve the definition first: if the latch must pass through the opening, excluding it does not answer the customer's fit question, even if the body measurement is repeatable.
Next, ask whether the shelf opening itself varies and whether the crate changes shape under the intended conditions. The required clearance is a relationship between mating items, not an isolated catalog dimension. A competent designer should determine appropriate limits. Buying staff can supply the actual use case, representative fixture information and consequences of poor fit without inventing an engineering tolerance.
When two reports disagree near a limit, preserve the identified part and request the setup details from both parties. Check units, reference points, assembly state and the agreed reporting rule before requesting another reading. If the methods match but the disagreement remains material, use the previously agreed specialist review process. Repeating measurements until one falls inside the tolerance is not a valid corrective action.
After resolving the issue, revise the method sheet if clarification was needed and retain the earlier report with an explanation. Tell every inspection provider which revision now applies. A transparent history is useful when a later order is assessed by different staff. It also prevents a one-time concession from being mistaken for a permanent change in the product requirement.
More practical specification questions are available in the product sourcing archive. Keep the dimensional requirement alongside its functional reason so future cost-reduction work does not remove a feature whose importance is otherwise invisible.
Frequently Asked Questions
Why can a supplier and an inspector report different dimensions?
They may use different reference points, product states, contact forces, equipment or rounding rules. Material flexibility and measurement uncertainty can also contribute. Compare the methods and original observations on the same identified sample before concluding that one party's report is wrong or misleading.
Is a digital caliper always the best tool?
No. Tool choice depends on the feature, range, tolerance and material. A caliper can distort a flexible part or miss a functional relationship. Ask a qualified provider to select a suitable measurement method and explain why it supports the intended acceptance decision.
Does calibration mean every measurement is correct?
No. Calibration information is one part of a suitable measurement process. Positioning, sample condition, operator technique, environment and uncertainty still matter. Review how the equipment is used for the actual feature, rather than treating a calibration certificate as a complete inspection method.
Should a buyer tighten tolerances to improve quality?
Only when the application requires it and the manufacturing and measurement processes can support it. An unnecessarily tight tolerance can increase cost and disputes without improving customer function. Define the functional need first, then agree technically justified limits and suitable verification with the supplier.
What should happen if a result is close to the limit?
Use the decision rule agreed before inspection, including the relevant treatment of uncertainty. Preserve the sample and records if review is needed. Do not change the acceptance rule retrospectively or select repeated readings solely because they produce a preferred outcome for the shipment.
Related KudBo Resources
Browse the KudBo product catalog, explore the buyer guide library, read more Wholesale Buying sourcing guides, or send your product requirements for a focused sourcing discussion.
Conclusion
Dimensional agreement begins with a shared method. Define the functional requirement, show the measurement locations, control sample condition and select appropriate equipment. Resolve borderline decisions before inspection and retain the observations needed to investigate differences. These steps make supplier discussions more concrete and help buyers distinguish a measurement problem from a product problem.
Final CTA
Request a Sourcing Review. Browse the KudBo product catalog and buyer guide library, then email the application and dimensional requirements to info@kudbo.com. Include your drawing revision and intended inspection approach so the discussion can focus on a clearly defined product requirement.