Introduction
Retail-ready packaging is not automatically better packaging. It is a controlled system intended to move a product from warehouse to shelf with less handling and clearer presentation. For an importer, the decision is commercial and operational: does the retailer need shelf-ready outer cases, does the product need a separate consumer pack, what will protect it through the route, and who owns the pack-out data? Answer those questions before asking a factory for “premium packaging.”
Define the Retailer’s Actual Requirement
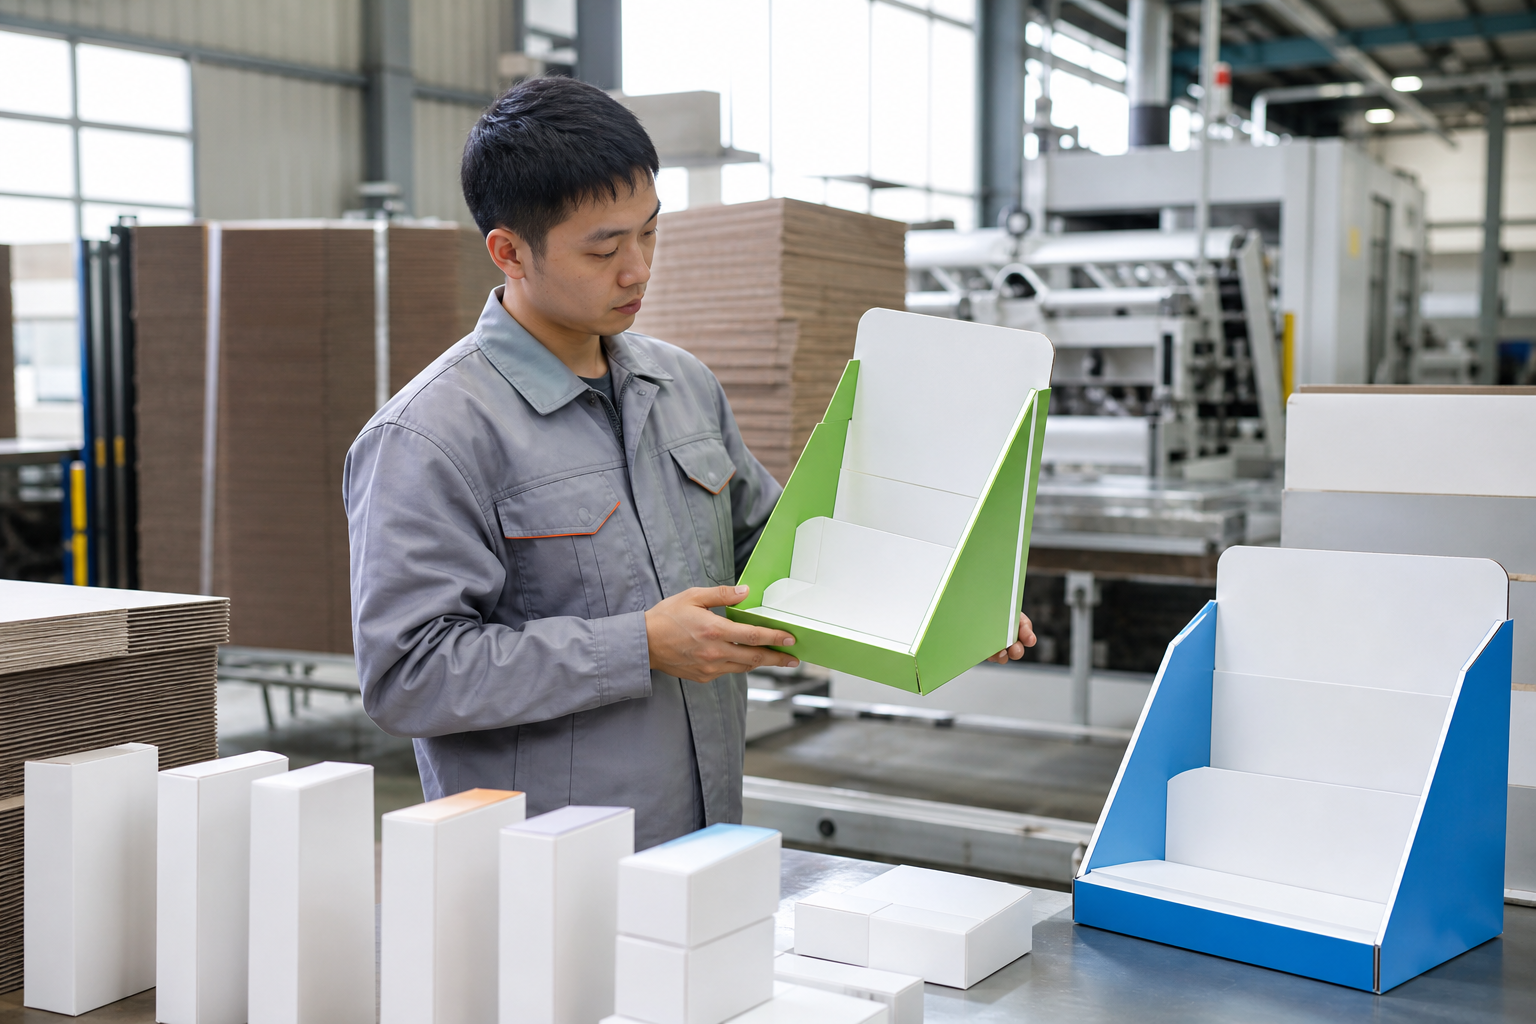
Ask the buyer or retailer for its delivery manual, packaging hierarchy, shelf dimensions, case count, barcode data, opening method, display constraints, recycling or material policy, maximum carton dimensions and inbound handling expectations. Do not build a shelf-ready case from an image alone. A club-store tray, retail-ready case, counter display, ecommerce mailer and export master carton have different jobs.
Translate the request into an RFQ table: product SKU, unit pack dimensions, retail case dimensions, units per case, case-opening sequence, display face, replenishment method, material specification, print requirement, pallet plan, shipment route, maximum weight and acceptance evidence. The FEFCO technical documents are a useful reference for corrugated-case terminology and design communication, but they do not replace a retailer’s own specification.
Choose the Packaging Hierarchy
Separate the consumer unit, inner pack where used, shelf-ready case, master carton and pallet. One box rarely performs every role well. A consumer unit may need a product image and instructions; a shelf-ready case may need quick opening and shelf presentation; an export master carton may need stacking and handling strength. Combining them can reduce materials in one situation and create damage or costly rework in another.
For a lightweight desk accessory, the unit pack and case might be simple. For a fragile digital microscope, internal protection, tray geometry and carton strength can be more decisive than surface graphics. Agree the actual packed product weight and center of gravity before deciding inserts.
Make Opening and Replenishment Testable
Define how staff open the case, remove waste, identify the product and place it on shelf. A perforation that looks good in a sample can tear poorly after humidity exposure or transit compression. A display lip can obscure product identity. A quick-opening case can expose the product if there is no retention feature. Ask for a physical packaging sample and test the intended handling sequence with representative product weight.
Record what was tested: sample revision, product count, operator action, observation and deviation. Avoid broad claims such as “retail proven” unless there is evidence for the exact configuration and channel.
Mid-Article CTA
Planning retail-ready packaging for an imported product range? Browse KudBo products and email info@kudbo.com with your retailer manual, SKU list, expected pack count and destination. We can coordinate product samples, packaging concepts and factory-side shipment evidence.
Plan Protection Around the Distribution Route
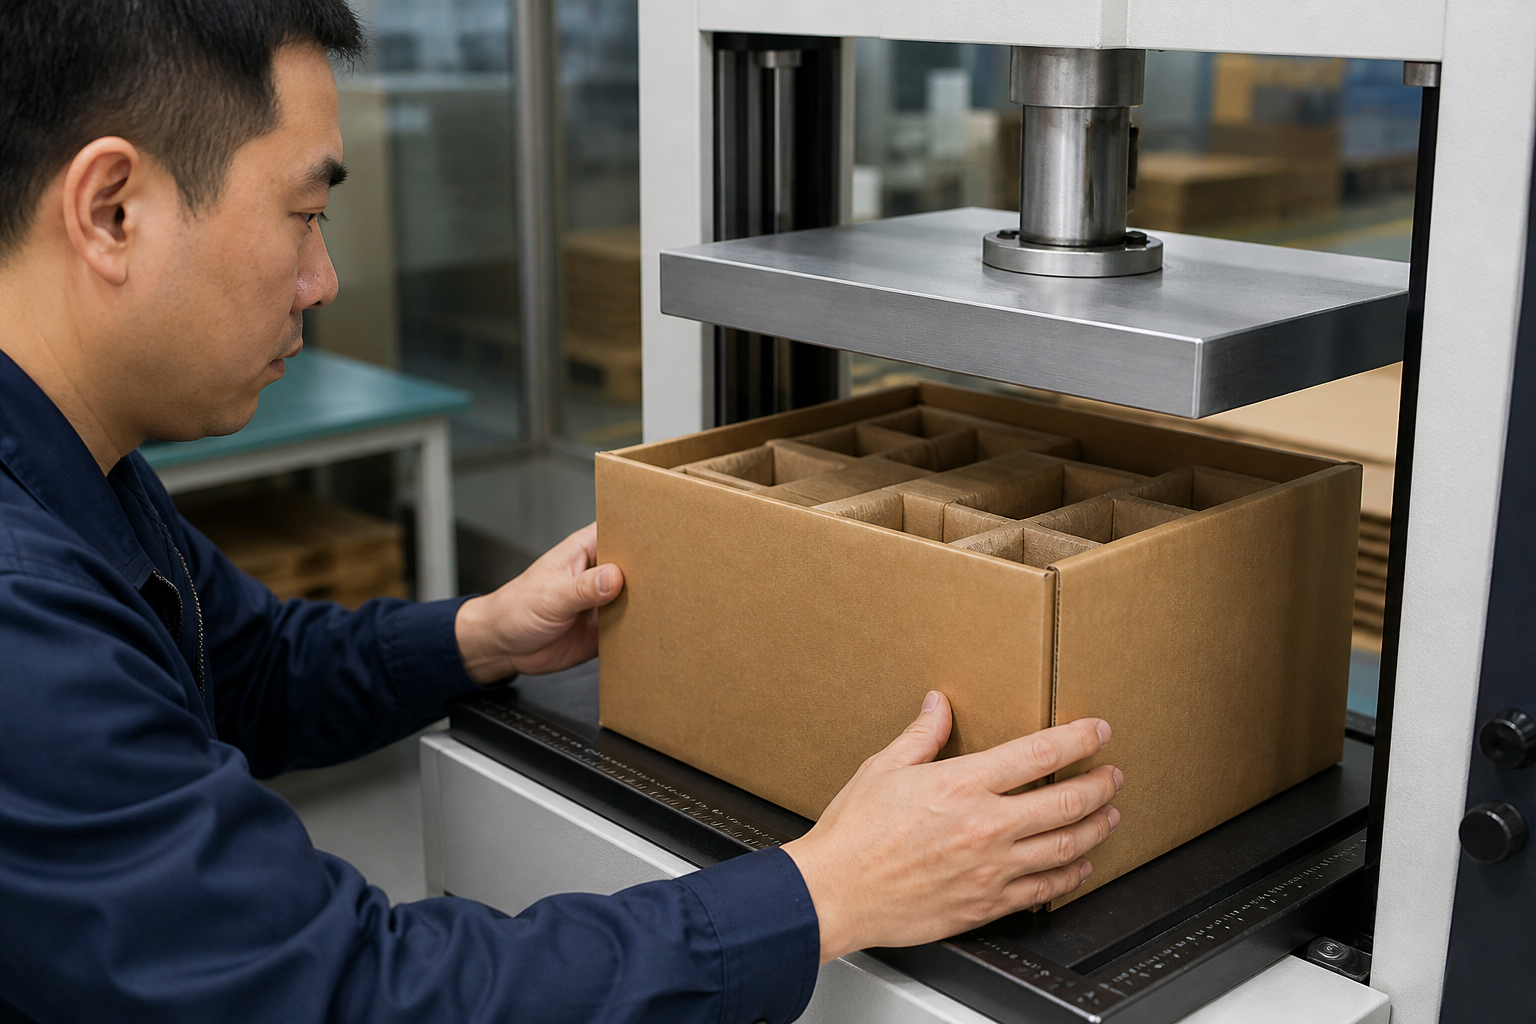
Package design should consider factory handling, consolidation, container loading, port movements, warehouse storage, pallet stacking and retail replenishment. Define orientation, void fill, edge protection, sealing, pallet pattern and moisture risks as appropriate. If you request package testing, agree the exact test plan, sample configuration and success criteria before testing starts.
ISTA test procedures provide recognized test frameworks, but an ISTA procedure is not a generic claim of durability. The report must identify the complete packed product and tested configuration. A redesigned insert, changed product weight, new carton board or different pack count can change the result.
Factory Production Controls
Before production, approve structural dielines, material specifications, print proof, pack-out drawing and retained sample. At first-piece review, verify dimensions, board grade or agreed material, opening function, product fit, barcode location, color reference, protective parts and unit count. At pre-shipment inspection, sample across the lot and check the same points on completed goods and cartons.
Log carton dimensions and gross weight on finished goods. Count inner packs, outer cases and pallet totals separately. If carton compression, drop or transit testing is part of the plan, preserve the report and samples in the order file rather than relying on a marketing statement.
Compare Quotes on Equivalent Scope
When packaging suppliers quote different materials or structures, compare packed dimensions, unit count, board specification, print coverage, inserts, finishing, assembly, tooling, waste allowance, test scope, lead time, palletization and correction responsibilities. A lower carton price may create higher freight, damage or retail-labor cost. Ask for a quantified assumption instead of accepting vague “strong carton” language.
Also plan artwork and sustainability claims carefully. “Recyclable” may depend on material, construction, local infrastructure and market rules. Use accurate, supportable wording approved by the responsible party.
Frequently Asked Questions
Is shelf-ready packaging necessary for every retail product?
No. It is justified when the retailer’s handling and presentation requirements support the added structure and cost.
Can one package serve ecommerce and retail?
Sometimes, but compare route protection and presentation needs rather than assuming one format will work for both.
What should be checked at shipment inspection?
Check agreed dimensions, unit count, product fit, opening function, visible artwork, protection, carton condition and pack-out against the approved sample.
Does a corrugated box code prove carton performance?
No. Material and design terminology support communication; route-specific performance still needs appropriate validation.
When should carton dimensions be finalized?
After the finished product and protective components are packed in the approved production configuration.
Prototype Before You Commit to Tooling
Use a structural sample for the actual product weight and accessories, not an empty presentation mockup. Open it, lift it, place it on a shelf, remove one unit, return it to a case and observe where it tears or becomes confusing. If a retailer will handle the case in a particular way, include that sequence in the review. Record material, dimensions, opening feature, unit count, operator feedback and any revision request.
The packaging designer, factory and buyer should agree what the sample proves. A hand-made prototype can confirm fit and opening logic, but it may not reproduce production board, glue, die-cut tolerance, printing or transit performance. Use a production-representative sample before final approval and identify the retained sample with a date and revision.
Balance Labor, Freight and Damage Risk
Retail-ready packaging can reduce shelf labor but increase the factory packing steps, materials and carton cube. Compare the entire delivered system. Include unit and case materials, assembly labor, tooling, warehouse handling, pallet efficiency, freight volume, damage allowance and retailer acceptance. The lowest packaging unit price is rarely the only meaningful number.
For an ecommerce-plus-retail program, model at least two options: a protective consumer unit inside a shelf-ready case, and a consumer unit designed to ship directly with a separate transit solution. Test both with the actual product, expected transport route and retailer specification. Select the option that makes the fewest unsupported assumptions, not simply the most visually elaborate display.
A Clear Acceptance Standard for the Factory
Write measurable requirements: board/material specification, dimensions and tolerance, unit count, opening sequence, product fit, visible print reference, barcode position, acceptable cosmetic defects, pallet pattern, gross weight and evidence photos. Add a defect classification for packaging where it matters. A torn perforation that prevents shelf use may be major; a small non-visible carton mark might be minor. Definitions should be agreed before inspection.
During shipment inspection, sample cases from different carton positions and record product fit, opening, count and visible defects. When a test is destructive, decide in advance how many samples may be used and how replacement stock is handled. This gives both buyer and factory a repeatable decision process instead of a subjective argument at loading time.
Translate the Retailer Manual Into a Requirement Matrix
Retailer manuals can mix mandatory limits, recommendations, category rules and booking procedures. Extract only the clauses relevant to the planned product and route. For each, record the source section, requirement, product or packaging level, design response, verification method, owner and approval status. Keep the dated source file because retailer guidance can change.
Resolve conflicts before design. A retailer’s maximum case weight may clash with the buyer’s preferred pack count; shelf depth may conflict with the protective insert; barcode placement may sit on the proposed tear-away panel. Present the buyer with alternatives and their labor, cube and protection effects rather than asking the factory to choose silently.
Give the factory a short released specification derived from the matrix. The buyer should retain the original manual and interpretation record. This keeps production instructions usable without losing the basis for each decision.
Engineer the Opening Feature for Production Variation
Perforation length, nick spacing, board direction, die condition, coating, glue location and humidity can all change opening behavior. Define the desired sequence and unacceptable outcomes: uncontrolled tearing, exposed sharp board edges, product ejection, blocked branding, collapsed display wall or excess waste remaining on shelf.
Review samples after realistic conditioning and handling selected by the packaging specialist. Have several people perform the opening action because one designer familiar with the prototype may compensate for a weak feature. Record operator, sample, material and observation. A pass should refer to the agreed acceptance criteria, not “opened fine.”
On the production line, check first pieces from the actual die and board. Monitor die wear and glue placement at defined intervals. If operators need knives or unusual force to open the case, stop and compare with the approved sample.
Model Pallet and Shelf Efficiency Together
Case dimensions affect pallet utilization, freight cube, warehouse stability and the retail shelf. Create a layout using final external dimensions and allowable pallet height and weight. Check overhang, underhang, interlocking, compression paths and access for labels. Ask the logistics partner whether the plan suits the real route and equipment.
Then simulate shelf placement. Confirm the display face, number of facings, product removal, restocking, remaining product stability and whether the tear-away edge hides required information. A case that packs a pallet efficiently can still waste shelf space; a dramatic display can create poor container utilization.
Compare scenarios with explicit quantities and assumptions. Small changes to case count can affect both replenishment labor and freight. Do not claim savings until actual rates and handling inputs are available.
Approve Print and Structural Elements Separately
Structural approval should lock dimensions, material, folds, perforations, glue, insert and pack-out. Graphic approval should lock dieline version, color references, barcodes, claims and required information. Join them through a final imposed proof, but preserve the two approval histories.
This prevents a marketing copy correction from concealing an unapproved structural change. It also helps when a plain case and a printed case use the same construction. If a printer adjusts the dieline to fit its equipment, route the structural effect back to the packaging engineer.
At shipment inspection, compare both dimensions and artwork. A visually accurate case can use the wrong board or perforation; a structurally sound case can carry an obsolete barcode or claim. Report each defect in the appropriate category.
Plan Store Handling and Disposal
Ask what store staff do with tear-away panels, lids, straps, bags and protective inserts. Too many loose pieces can shift labor rather than reduce it. Where a component remains with the display, verify that it does not obstruct products or create an unstable edge. Where it is discarded, consider the retailer’s material and disposal policy.
Environmental claims need their own evidence and market review. A board grade or recycling symbol does not automatically prove that the complete pack is recyclable in every location, especially when it includes lamination, windows, foam, adhesives or mixed-material inserts. Use precise material descriptions and approved claims.
Customer experience also matters. If shoppers remove individual units from the case, check that remaining packs stay upright and that required product information is visible. Store-ready design should support real handling, not only a staged photograph.
Close the Loop After the First Delivery
Collect structured feedback from the retailer, warehouse and customer-service teams: case damage, opening time, shelf presentation, replenishment, barcode access, product damage and waste. Separate isolated handling events from repeated design problems. Ask for photographs and shipment or lot references where possible.
Route findings into the next reorder’s change control. A thicker board may affect die cutting, dimensions, cost and pallet count; an altered display lip may affect artwork and barcode visibility. Update the retained sample and acceptance standard after approval, and remove the previous version from production.
The first delivery is the best source of experience for the second. Use observed facts without inventing performance percentages or claiming retailer endorsement.
Build a Costed Packaging Decision Record
For every shortlisted structure, record the annual or order quantity, unit material cost, tooling, assembly labor, packed cube, pallet count, estimated damage assumptions, store handling steps and waste components. Mark all estimates and name their source. Avoid presenting an untested damage allowance or labor saving as a proven result.
Ask the retailer and logistics partners which costs they bear and which are charged back to the supplier or importer. A design that saves shelf labor may require a higher factory assembly cost; a smaller case may improve cube but increase replenishment frequency. The decision should show the tradeoff the buyer accepted.
After the first delivery, replace assumptions with observed data where available. Keep the same structure if it performs adequately; redesign only when a measurable requirement or recurring issue justifies the change. This disciplined record helps future buyers understand why the pack looks the way it does.
Document the final decision in the SKU file with approved samples, dielines, board specification, pack-out photographs, pallet plan, retailer sign-off where provided and unresolved limitations. On every reorder, confirm that product weight, case count, board source, print supplier, route and retailer manual are unchanged. This short reconfirmation prevents a purchasing substitution from undoing the packaging work.
Give warehouse and retail teams a simple feedback code for crushed cases, failed perforations, unstable displays, blocked barcodes and missing units. Consistent categories make first-delivery observations comparable with factory inspection records. Do not turn a single store photograph into a performance rate; investigate the lot, route and handling context before changing the approved structure.
Related KudBo Resources
Browse the KudBo product catalog, explore the buyer guide library, read more Packaging & Shipping sourcing guides, or send your product requirements for a focused sourcing discussion.
Conclusion
Retail-ready packaging works when retailer handling, product protection, structural design and factory controls all point to the same finished case. Turn those needs into a measurable RFQ and inspect the shipped configuration—not a presentation-only sample.
Final CTA
Browse KudBo products, read our ecommerce packaging article, or email info@kudbo.com with your retail packaging brief.